Turnkey Solutions
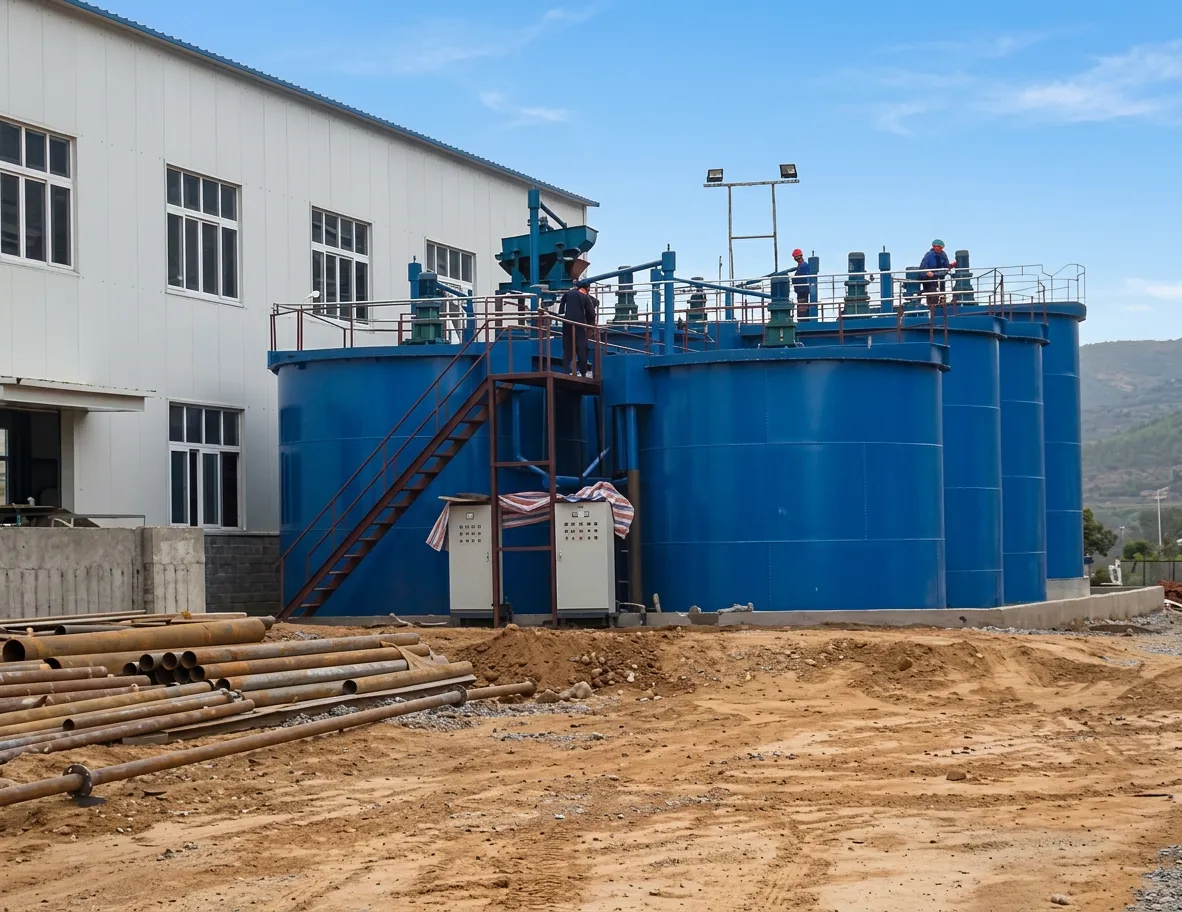
Integrated mineral processing plants from design to commissioning. We provide complete production lines for gold, copper, iron, lithium, and other metallic and non-metallic ores.
.jpg)
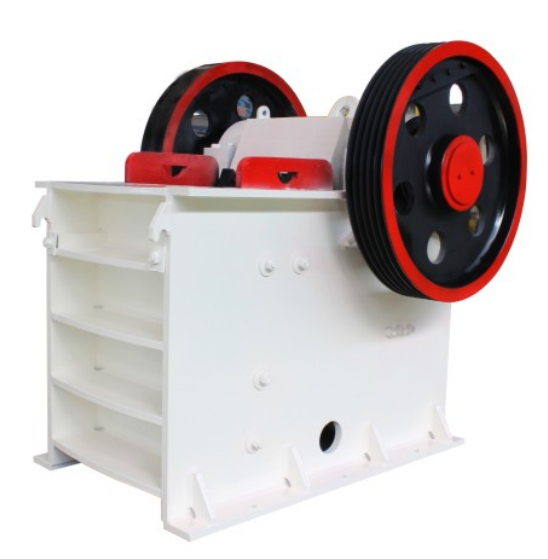
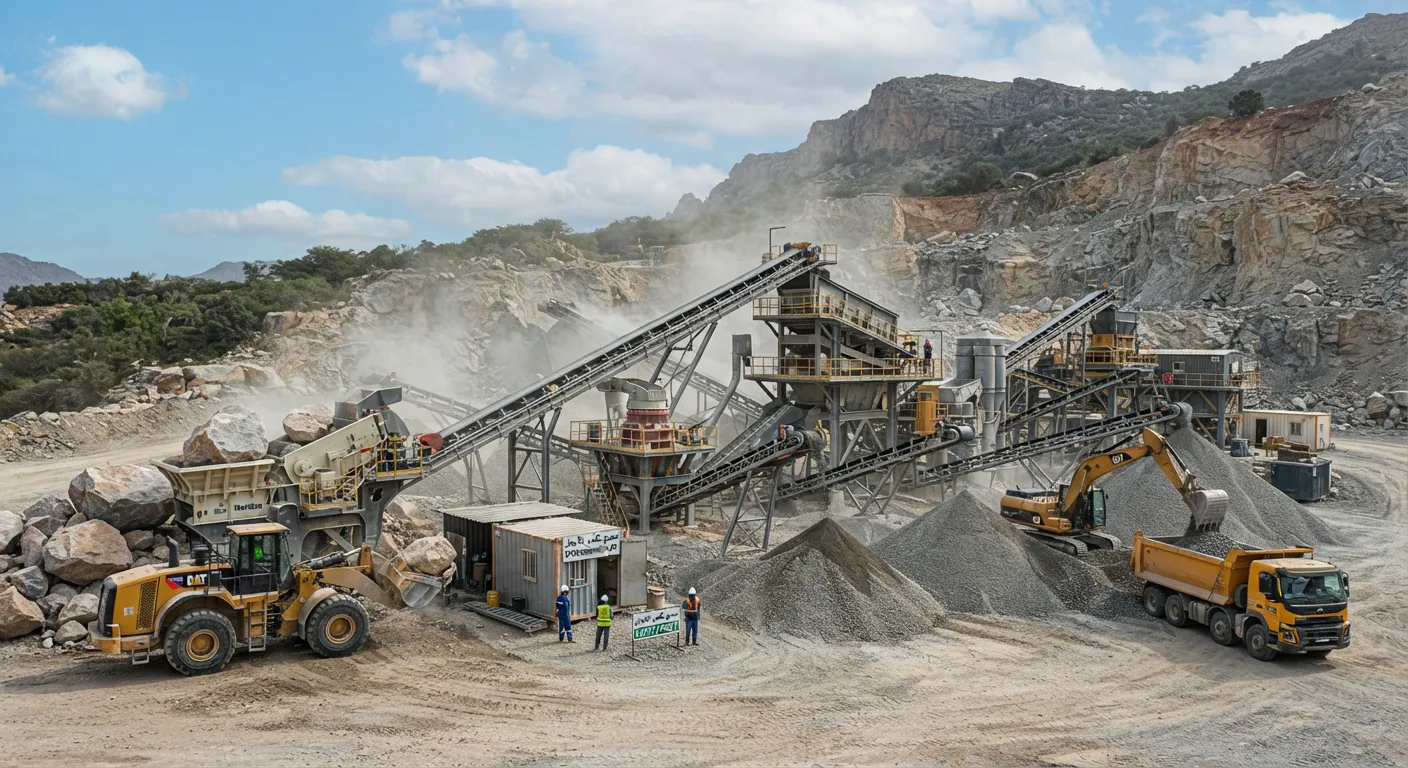
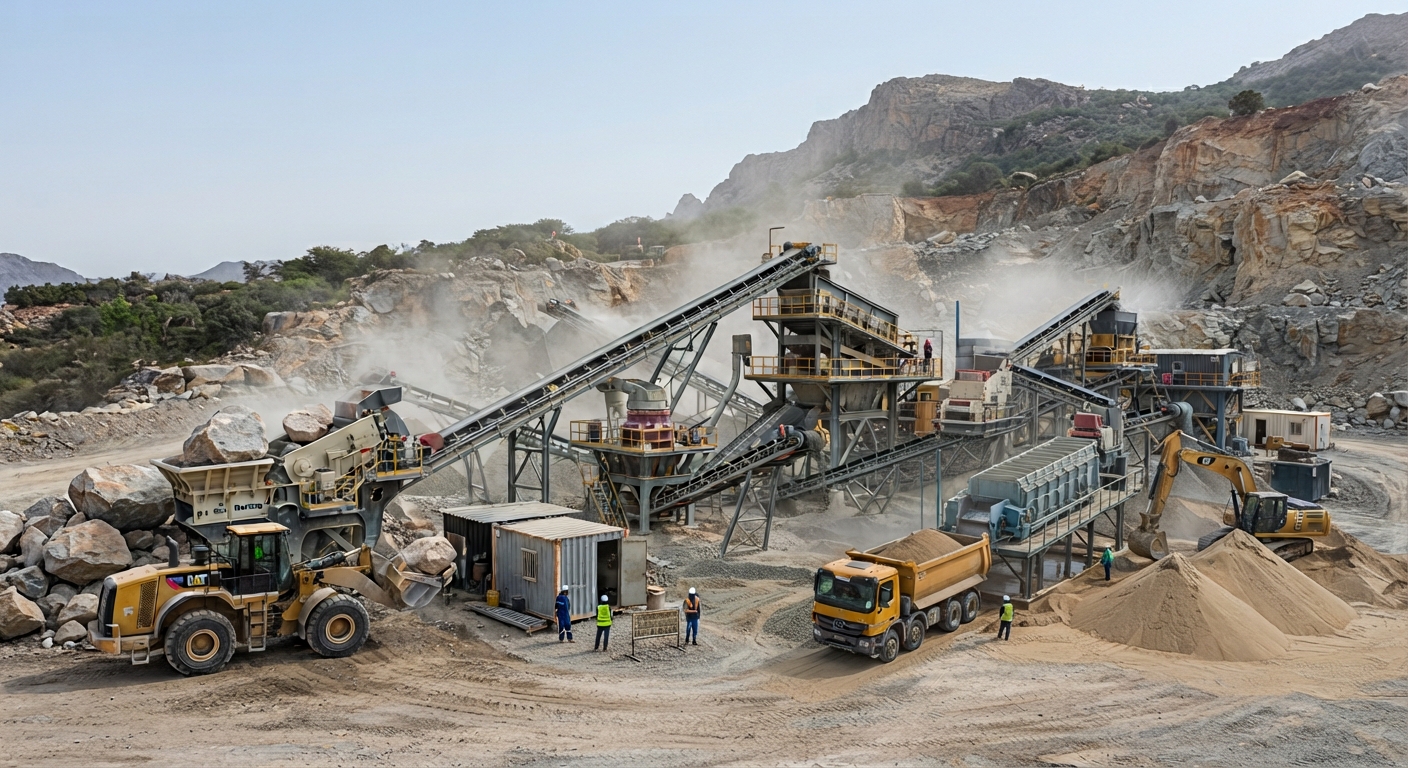
Stone Crushing Plant
Complete stationary and modular crushing plants for granite, basalt, limestone, and hard rock aggregate.
Capacity
50 - 1000 t/h
Recovery
100%
.jpg)
Sand Making & Shaping Plant
Advanced manufactured sand production lines producing premium cubical fine aggregate with controlled fineness modulus.
Capacity
30 - 300 t/h
Recovery
95%
.jpg)
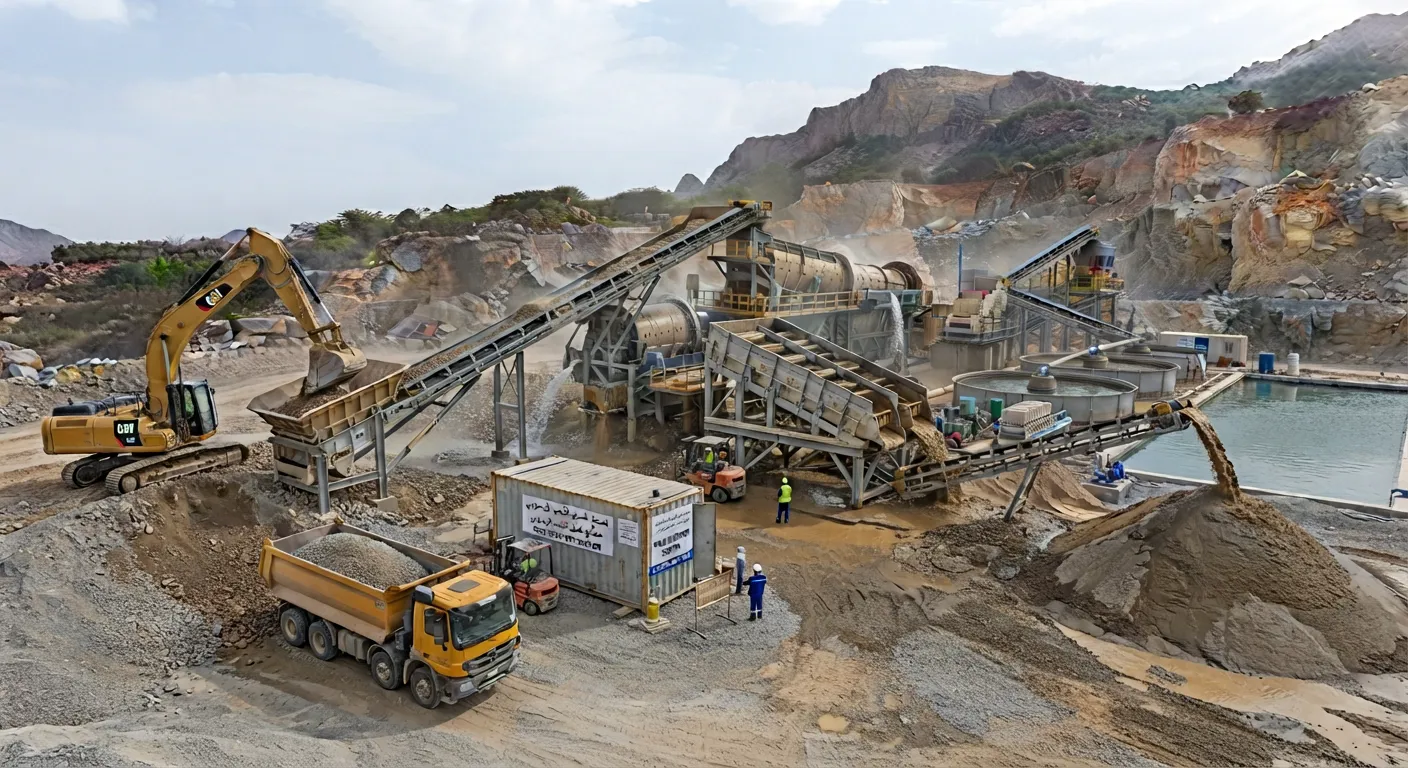
Sand Washing & Dewatering Plant
High-efficiency sand washing, desliming, and dewatering lines for producing clean, silt-free construction sand.
Capacity
20 - 250 t/h
Recovery
98%
.jpg)
Alluvial Placer Gold Washing Plant
Highly portable and trailer-mounted alluvial gold washing and gravity recovery plants for placer gold deposits.
Capacity
10 - 250 t/h
Recovery
92 - 98%
.jpg)
Hard Rock Gold Processing Plant
Complete crushing, fine grinding, gravity concentration, and flotation circuits for hard rock gold ores.
Capacity
5 - 100 t/h
Recovery
90 - 96%
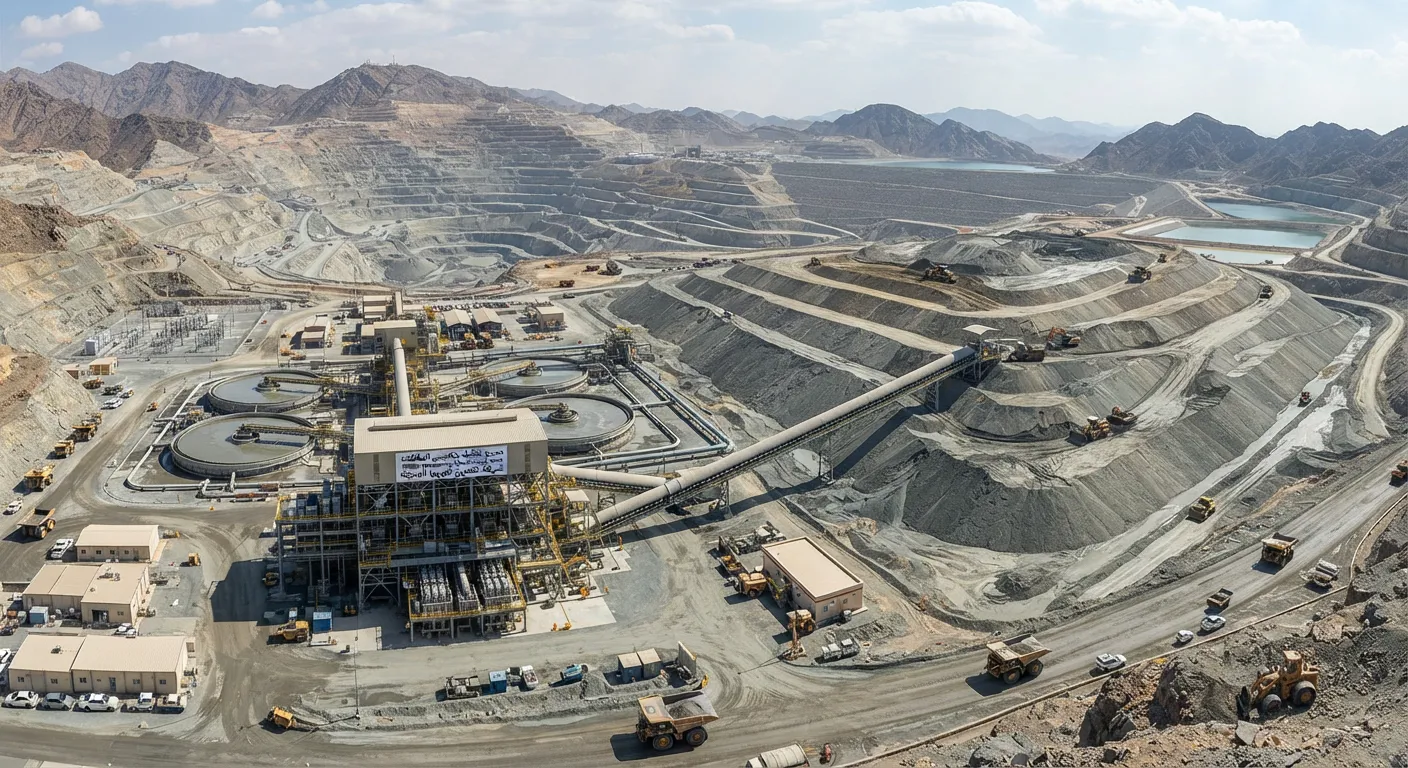
.jpg)
Gold CIL / CIP Cyanide Leaching Plant
Turnkey Carbon-in-Leach (CIL) and Carbon-in-Pulp (CIP) cyanidation plants for oxidized and refractory gold ores.
Capacity
50 - 500 t/d
Recovery
92 - 97%
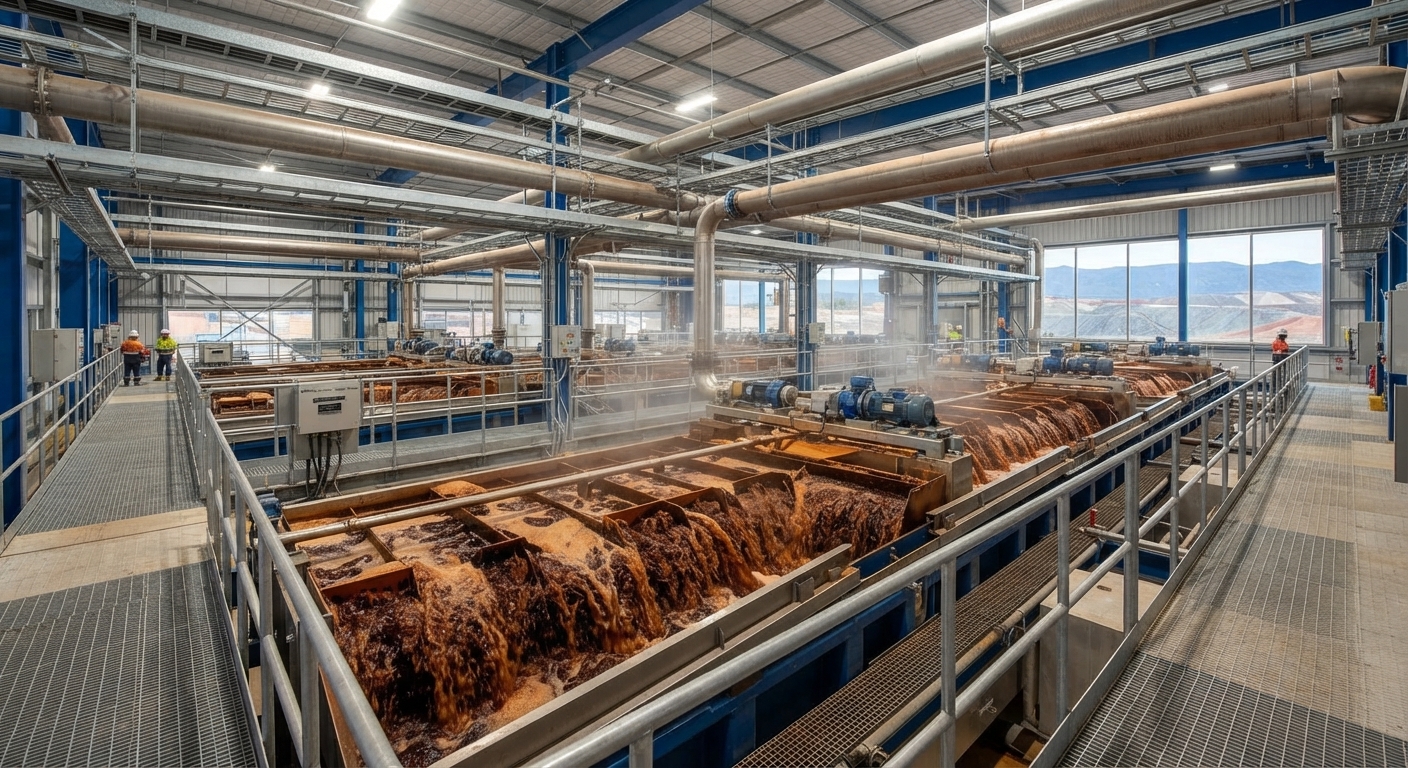
Copper Ore Flotation Plant
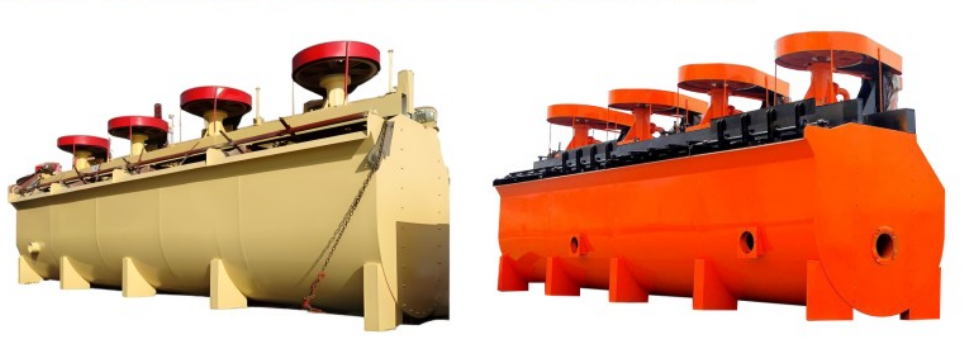
Comprehensive froth flotation processing plants for sulfide and oxide copper minerals with automated concentrate dewatering.
Capacity
50 - 500 t/h
Recovery
88 - 94%
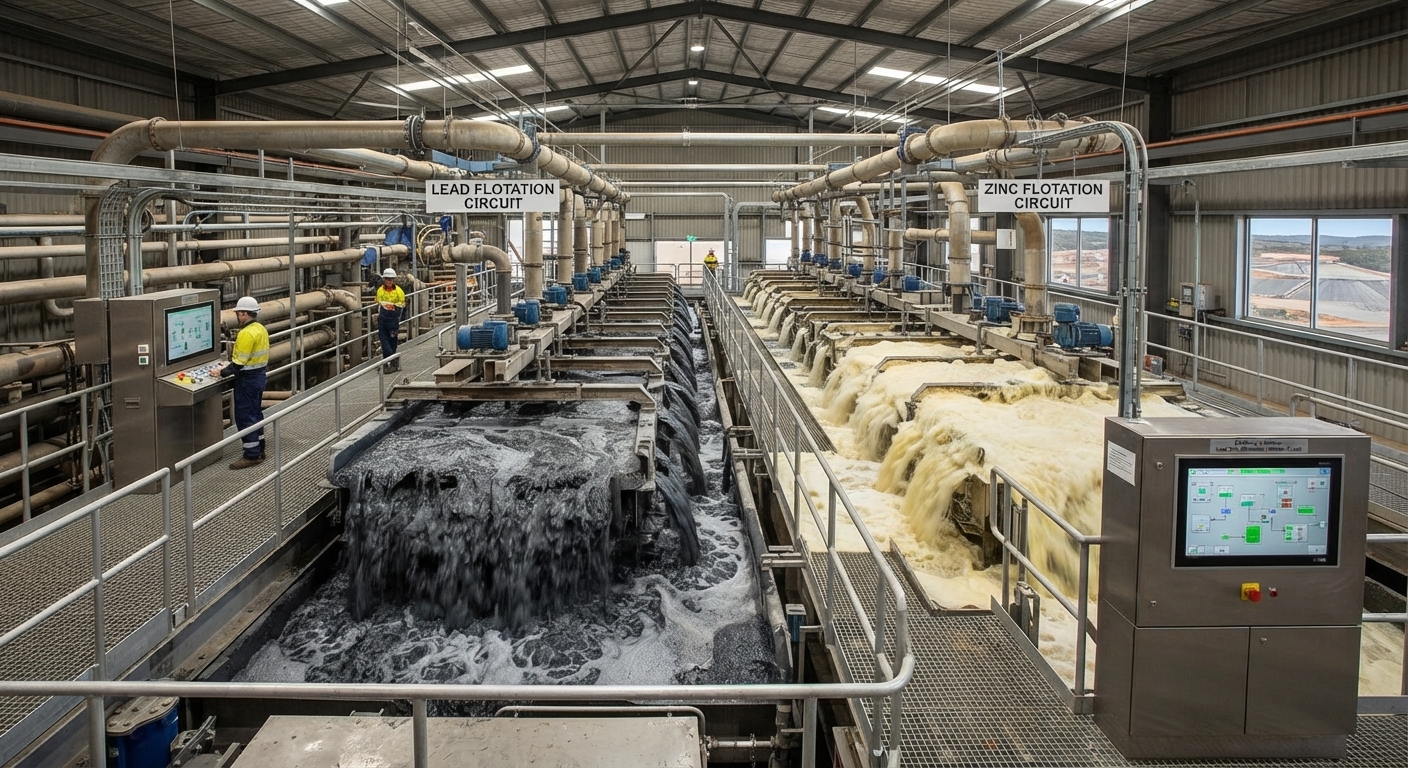
Lead-Zinc Differential Flotation Plant
Multi-stage differential flotation plants engineered for selective separation and recovery of high-grade lead and zinc concentrates.
Capacity
30 - 300 t/h
Recovery
85 - 92%
.jpg)
Tin & Tungsten Gravity Processing Plant
Eco-friendly gravity and high-gradient magnetic separation plants for cassiterite, wolframite, and scheelite beneficiation.
Capacity
10 - 150 t/h
Recovery
80 - 90%
.jpg)
Magnetite Iron Ore Processing Plant
Continuous wet magnetic separation plants upgrading low-grade magnetite into 65%+ Fe premium iron ore concentrate.
Capacity
50 - 600 t/h
Recovery
90 - 95%
.jpg)
Hematite & Limonite Beneficiation Plant
Advanced high-gradient magnetic and reverse flotation plants for weakly magnetic hematite and limonite ores.
Capacity
30 - 400 t/h
Recovery
82 - 88%
.jpg)
Chrome & Manganese Beneficiation Plant
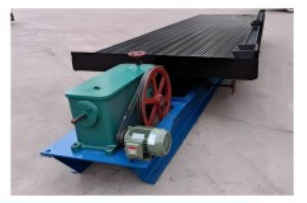
Washing, jigging, shaking table, and magnetic separation lines for lumpy and fine chrome and manganese ores.
Capacity
20 - 200 t/h
Recovery
85 - 92%
.jpg)
Silica Sand & High-Purity Quartz Plant
Scrubbing, classification, high-gradient magnetic iron removal, and dewatering lines for glass and foundry-grade silica sand.
Capacity
20 - 300 t/h
Recovery
95%
.jpg)
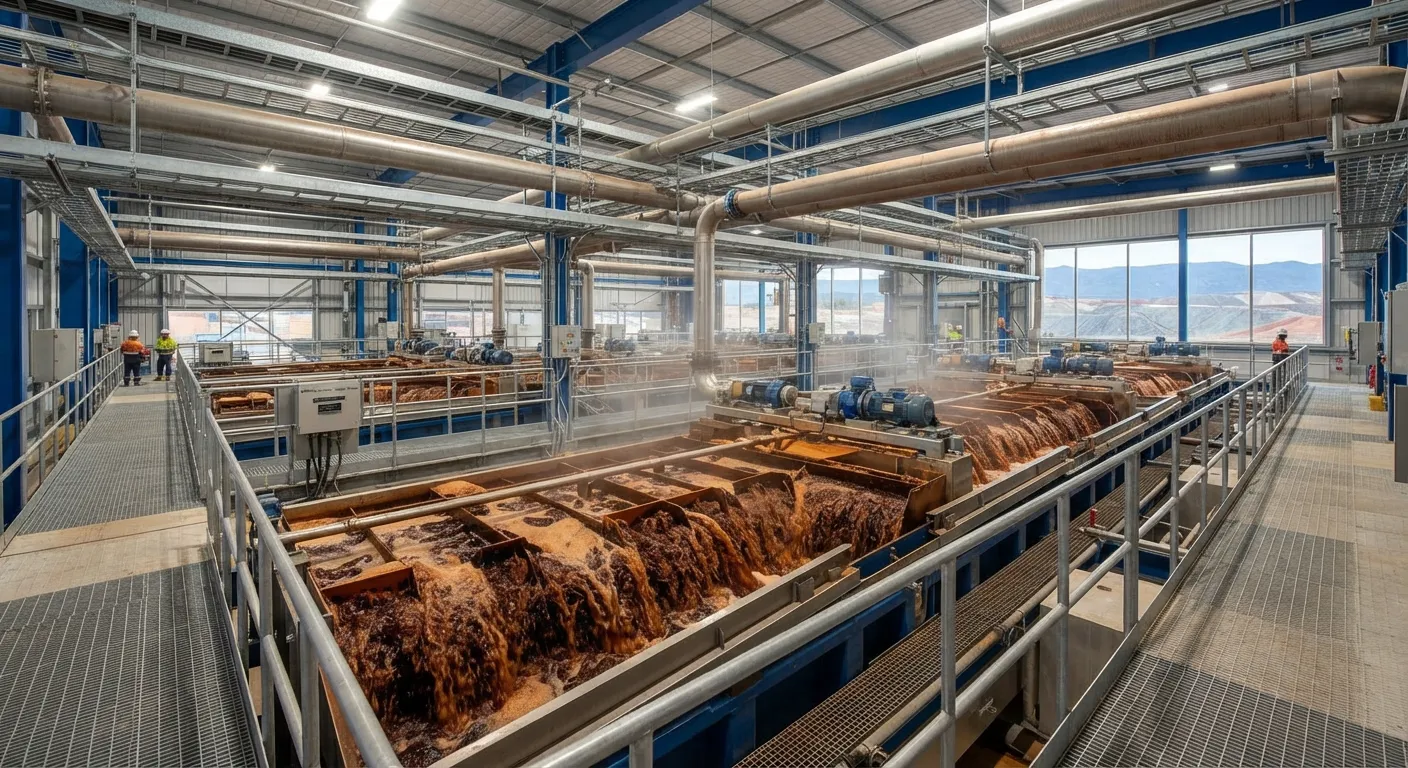
Tailings Dewatering & Dry Stacking Plant
Closed-loop zero-effluent tailings dewatering and dry stacking systems providing clean process water recycling and environmental safety.
Capacity
50 - 800 t/h
Recovery
95% Water Recycled
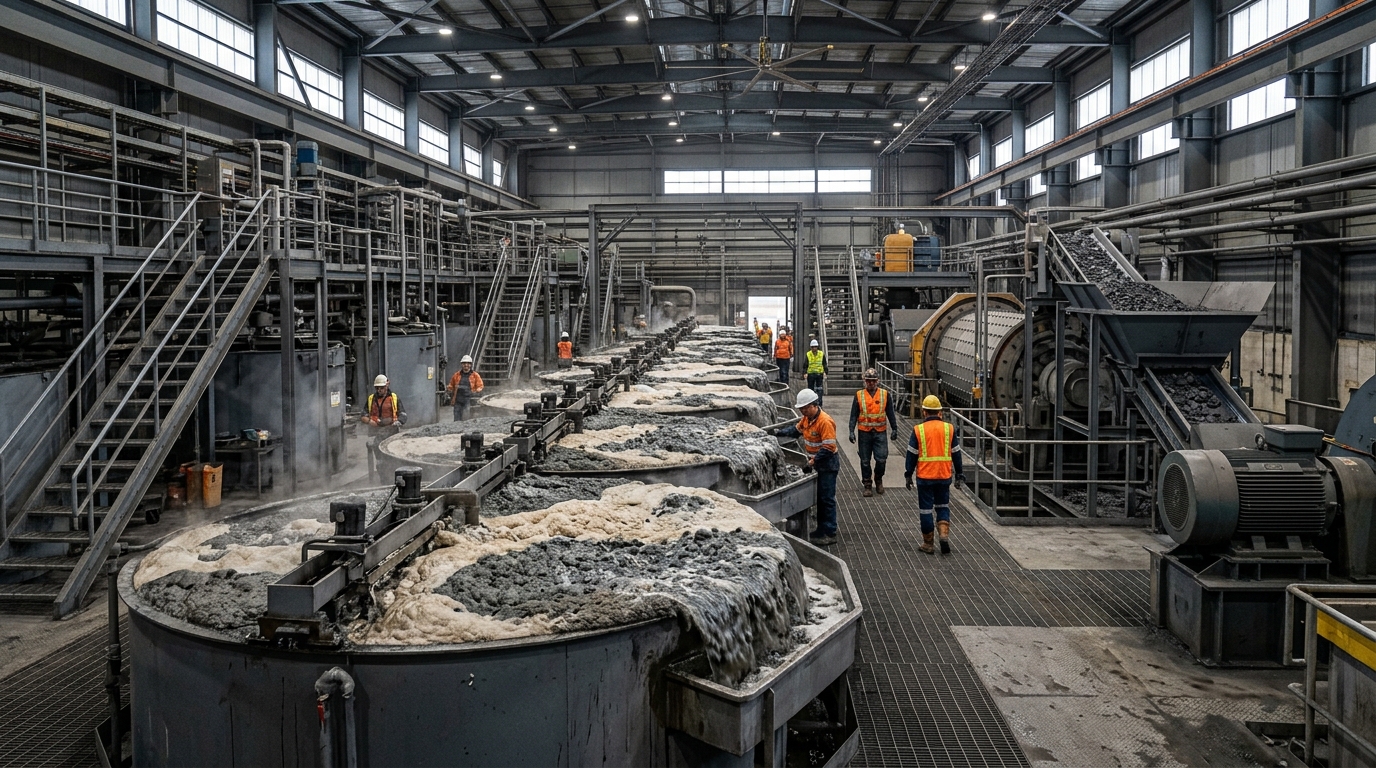
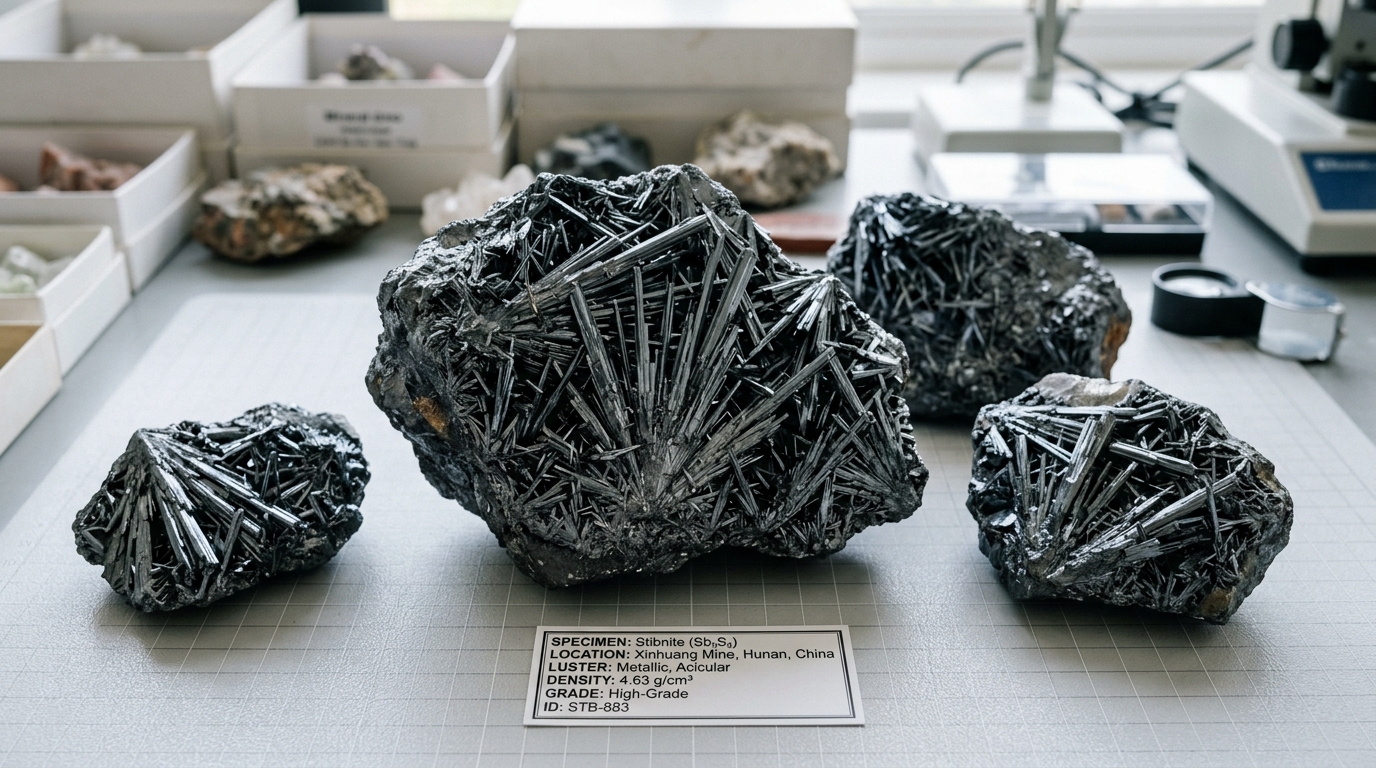
Antimony Ore Flotation Plant
Comprehensive differential froth flotation processing plants for stibnite (antimony sulfide) and complex ores, yielding high-grade 55-65% Sb concentrate.
Capacity
10 - 200 t/h
Recovery
88 - 94%
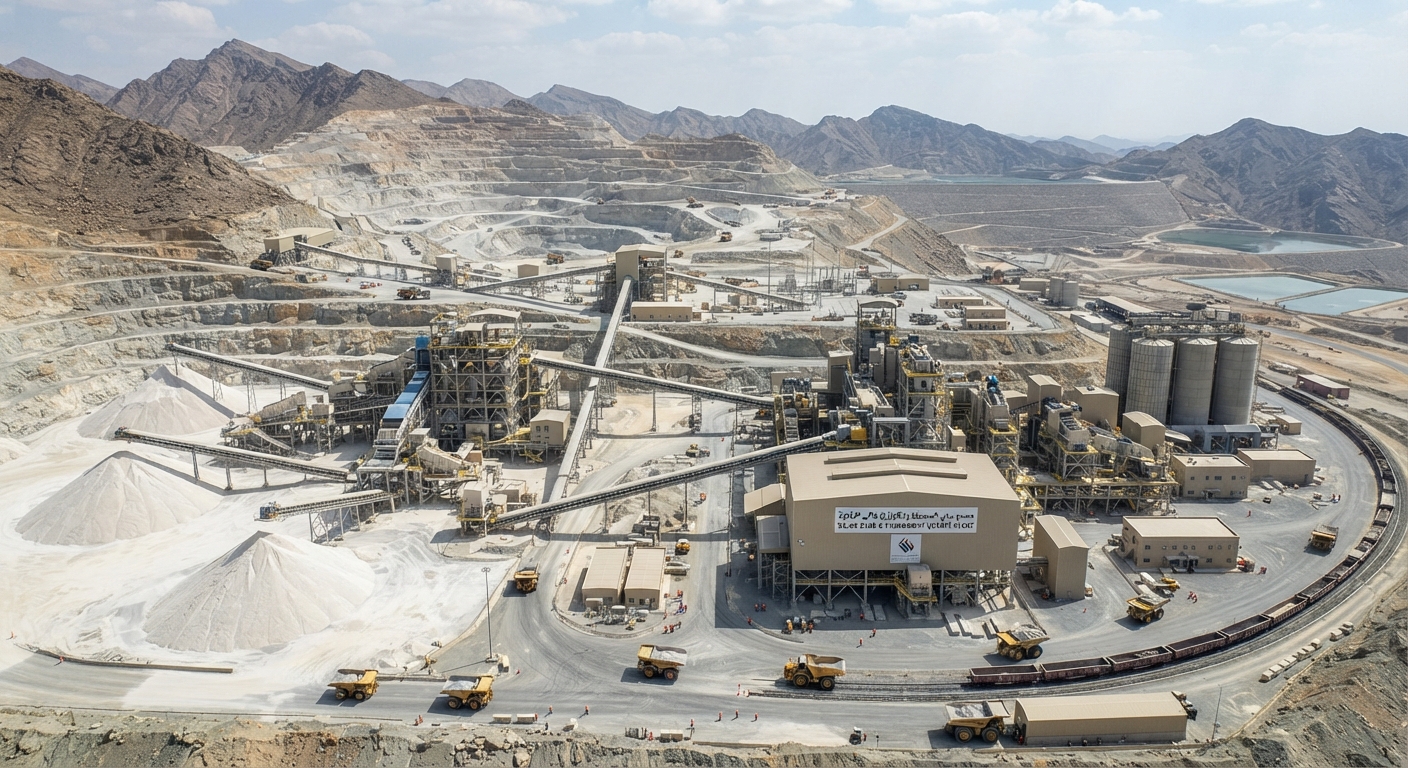
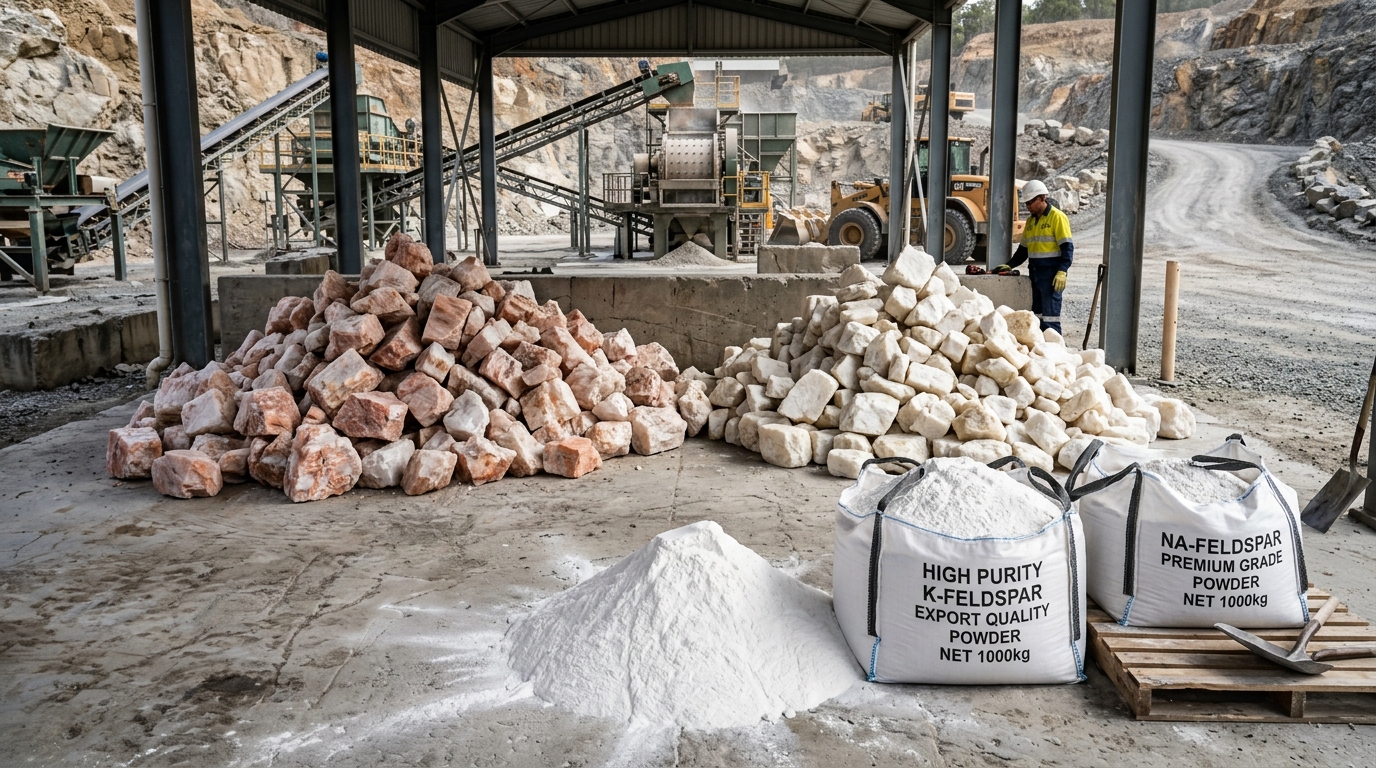
Feldspar Beneficiation & Magnetic Plant
Complete beneficiation, attrition scrubbing, and wet high-gradient magnetic separation plants for potassium and sodium feldspar, reducing Fe₂O₃ below 0.05%.
Capacity
5 - 100 t/h
Recovery
85 - 92%
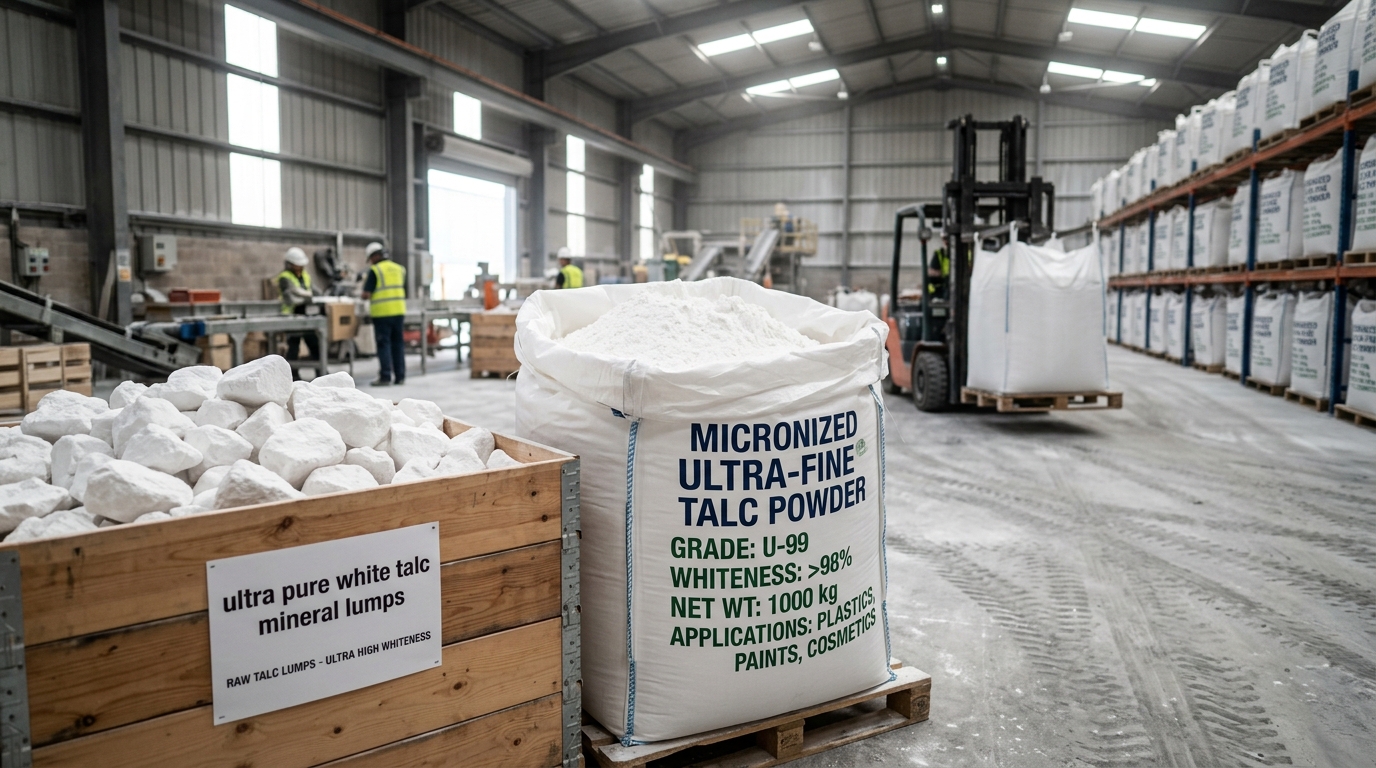
Talc Micronizing & Air Classification Plant
Turnkey ultra-fine dry grinding and dynamic turbo air classification plants delivering 325 to 2500 mesh asbestos-free micronized talc powders.
Capacity
1 - 20 t/h
Recovery
95 - 98%
Looking to Purchase Export-Ready Raw Ores Directly?
Alongside our turnkey EPC processing plants for non-ferrous and industrial minerals, ELMAGD MINING directly exports certified commercial-grade ores: Antimony Stibnite Lumps (63-65% Sb), High-Purity Feldspar (K & Na), and Asbestos-Free Egyptian Talc. Each cargo is backed by independent third-party inspection (SGS / AHK) with flexible FOB Egypt and CIF delivery terms.
Need a customized solution?
Contact our engineers for technical consultation and project evaluation.